
Plate Rolling Machine Operation: Tips for Better Rolling
A plate rolling machine is only as good as the operator using it. Even a high-quality hydraulic plate roller can produce oval cylinders, twisted cones, or flat spots if the setup and technique are wrong. Here are practical tips to get better results from your sheet metal rolling machine.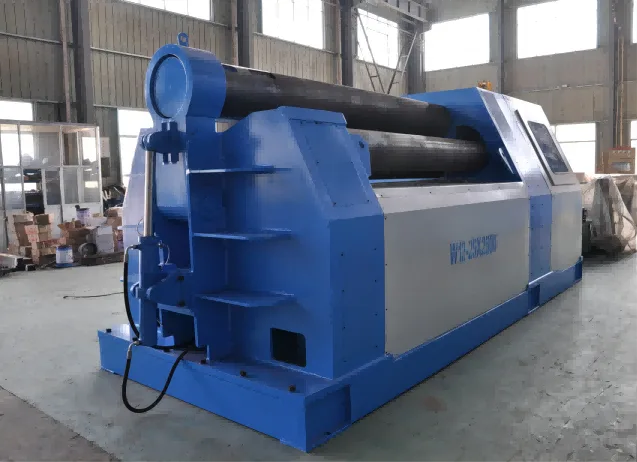
First, start with a square edge. The plate edge must be square to the length. A crooked edge produces a crooked cylinder. Second, use the pinch roll for pre-bending. Pre-bending the leading edge removes the flat spot that otherwise appears at the start of the roll. Third, make multiple passes. Rarely can you roll a cylinder in one pass. Take light passes and check the diameter frequently. You can always roll more, but you cannot unroll.
Fourth, watch for springback. Steel and stainless steel spring back after rolling. Over-roll slightly to compensate, then check the diameter with a template. Fifth, keep the rolls clean. Chips and scale on the rolls leave marks on the workpiece and affect rolling accuracy. Sixth, align the rolls correctly. Misaligned rolls cause spiraling and tapered cylinders. Check alignment regularly.
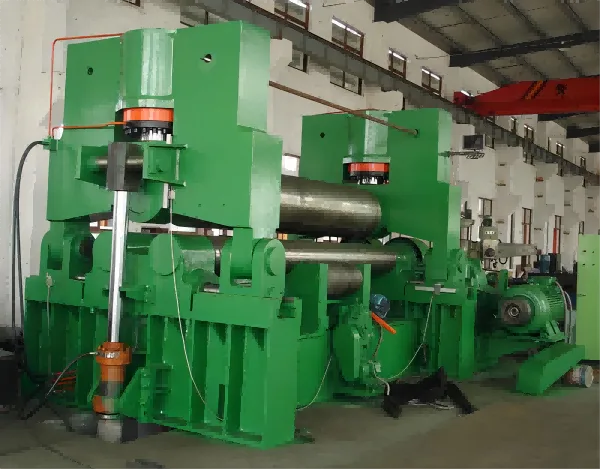
For cone rolling, set the rolls at an angle and feed the plate gradually. Cone rolling takes practice, but a 3-roll plate bending machine with adjustable rolls makes it easier. For production work, a 4-roll plate rolling machine with PLC control reduces operator error and improves repeatability. We supply plate rolling machines to customers in Saudi Arabia, Southeast Asia, and South America, with export packing and container loading.
Keywords: plate rolling machine operation, plate roller tips, hydraulic plate rolling machine, sheet metal rolling machine, cone rolling, plate bending machine, roll alignment, springback compensation.
Case Data:
A fabrication shop in South America reduced rejected cylinders by 50% after implementing three changes: pre-bending both edges, checking roll alignment weekly, and using a diameter template on every pass. The operator training took one day, and the improvement paid back immediately through less rework and faster delivery.
FAQ
Q1: How do I remove flat spots after rolling?
Pre-bend the leading and trailing edges before full rolling. On a 3-roll machine, this may require flipping the plate. A 4-roll machine pre-bends both ends in one setup.
Q2: How do I compensate for springback?
Over-roll slightly and check the diameter with a template. The amount of springback depends on material, thickness, and roll diameter. Experience and a trial piece help dial in the correct compensation.
Q3: How often should I check roll alignment?
Check alignment weekly for production work, or after any abnormal load or crash. Misalignment causes tapered and spiraled cylinders, which are difficult to correct later.


